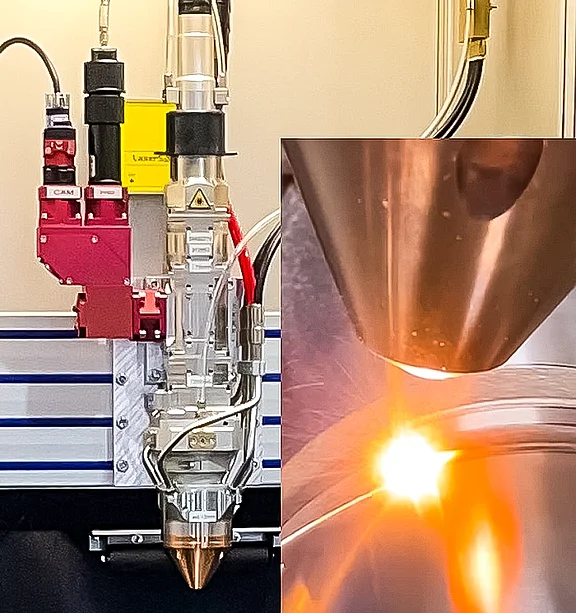
Example of laser cladding application
Precise temperature control improves the quality of the build-up welding processApplication example: Laser cladding
Precise temperature measurement and control facilitate the determination of process parameters and improve quality in LMD, AM and high-speed processes such as EHLA.
Customer Problem and Requirements
Laser power, powder mass flow and feed rate influence one another. Setting up a stable process often requires a significant investment of time and material until all the necessary parameters have been determined.
The Mergenthaler Solution
Process optimisation is based on temperature. Temperature, measured in °C, is a globally recognised standard and is therefore transferable. It serves as the key control variable for laser power.
In a coaxial configuration, the LASCON Process Controller looks directly at the molten pool through the optics — regardless of the direction of movement. The two-colour pyrometer integrated into the LPC04-2CDC measures the temperature at a high frequency in the kHz range, enabling a rapid response to process instabilities.
The controller compares the measured temperature with a predefined setpoint temperature. A typical starting value is the melting temperature of the material plus 150 K.
The controller, developed specifically for this application, calculates in real time by how much the laser power needs to be adjusted. This adjustment is transmitted directly to the laser source via an analogue 0–10 V signal. If the temperature rises – for example, due to heat build-up at the edges – the laser power is reduced. If the melt cools down, the laser power is increased.
The system responds within milliseconds. Coaxial or side-mounted MERGENTHALER LPC04 controllers regulate and monitor LMD and AM processes worldwide. The integrated monitoring tools oversee the entire process and ensure consistent quality.